Nous sommes responsables de la construction-----nous sommes responsables de la fabrication-----nous sommes responsables de la formation

Compare poinçonneuse à tourelle manufacturers on five checkable points: station count, drive type, forming capability, tooling standard and spare-parts lead time. Ask every supplier for the same data on each, then rank them against your own part mix instead of brand reputation.
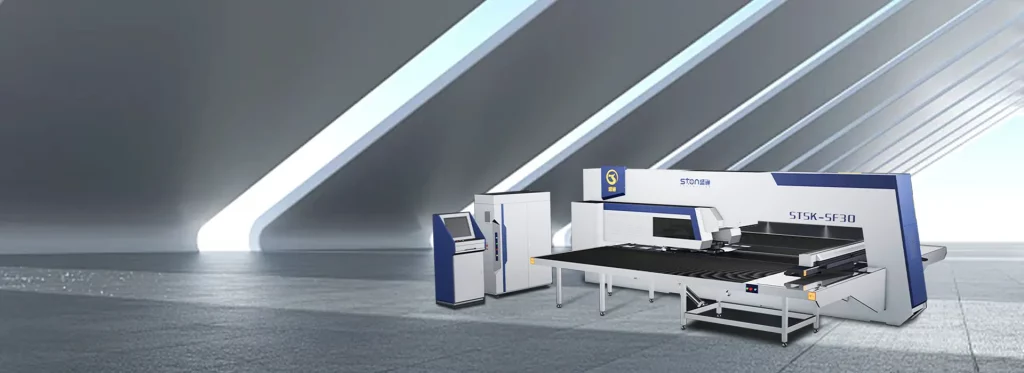
Search results for this term are mostly manufacturer brand pages and supplier directories. Each describes its own machines in its own vocabulary, so “turret speed” on one page and “hit rate” on another cannot go in the same column. This article supplies the column headings.
STON CNC, an original manufacturer with a 20,000 ㎡ self-owned factory in Qingdao, is used as the worked example, so you can see what a complete answer to each question looks like. STON is also a supplier you may be evaluating, so weigh the example accordingly.
| Criterion | Ask For | Why It Changes the Decision |
| Station Count and Layout | Station map by tool size, plus number of rotary stations | Decides whether your slot, louvre and angled jobs run without a tool swap |
| Drive Type | Turret speed, power draw, overload protection | Sets throughput per shift and electricity cost |
| Forming Capability | Forming tool list, max forming height per tool | Punching-only machines cannot take louvres or embossed features |
| Tooling Ecosystem | Tool interface standard, third-party compatibility | Controls the price and lead time of every replacement punch and die |
| Parts Lead Time | Response time, on-site time, wear-parts shipping time | Downtime cost usually exceeds the price gap between two machines |
Station count. A total number says little. What matters is how many stations of each tool size the turret holds and how many are rotary. STON’s SFL punch-laser machine lists its layout by size: 16 A, 11 B, 3 C and 2 D stations, including rotary stations 1B and 1C. The JT and SF turrets carry two rotary stations with independent control.
Drive type. STON’s turret range is mechanical, servo and punch-laser combined. The JT series uses a flywheel-driven mechanical system, and the SF series uses a servo drive. Hydraulic-drive turrets are outside the range covered here, so if a supplier quotes one, request the same data points and compare them line by line.
Forming. STON’s turret punch presses handle punching, forming and embossing. In the automated production-line configuration the turret also does trimming, louvering and rib pressing. Ask any supplier for the forming tool list and the maximum forming height with each tool, because forming loads the press differently from a plain punch.
Tooling. Le SFL machine runs long-guide 85 series international standard tooling. A standard interface lets you source consumables locally, while a proprietary one ties every replacement to a single vendor. Ask which applies before you compare machine prices.
Parts and service. STON states a 1-hour response, 48-hour on-site resolution, a dedicated spare-parts warehouse and lifetime tracking under a unique user ID, with free software updates. The mechanical JT series uses Panasonic and Siemens electrical components, which helps with local replacement. Ask each supplier for its own response, on-site and wear-parts shipping times in writing, so the three figures can be compared directly.
| Paramètres | JT (Mechanical) | SF (Servo) | SFL (Punch-Laser) |
| Vitesse maximale de la tourelle | 30 rpm | 40 rpm | Confirm with STON |
| Machining Accuracy | ±0.1 mm | ±0.1 mm | Not stated in this form |
| Capacité de charge maximale | 150 kg | 150 kg | Confirm with STON |
| Power Consumption | ≤2 kW | Approx. 3–5 kW | Confirm with STON |
| Air Pressure | 0.55 MPa | 0.55 MPa | Confirm with STON |
| Alimentation électrique | 380 V ±5% | 380 V ±5% | Confirm with STON |
| Control | Windows platform, RTEX bus servo; FANUC, Siemens or Rexroth on request | Same options | Integrated punch-laser CNC; FANUC optional |
| Punching Force | Confirm with STON | Confirm with STON | 300 kN (30 t) / 400 kN (40 t) |
| Cadre | Confirm with STON | Finite-element-optimized, narrow throat | O-type closed frame |
| Sheet Travel | Confirm with STON | Confirm with STON | X 2500 mm per position, up to 5000 mm with secondary positioning; Y 1250 / 1500 mm |
| Positioning Repeatability | Not stated | Not stated | ±0.01–0.02 mm (rack and pinion) |
| Tooling | Confirm with STON | Confirm with STON | Long-guide 85 series international standard |
The trade-off inside STON’s own range is speed against draw. The JT’s flywheel system holds electrical load at or below 2 kW but turns the turret at 30 rpm at most. The SF turns at up to 40 rpm and pulls roughly 3–5 kW. A shop running one shift of mixed small batches may never use the SF’s extra speed, while a shop running two or three shifts of repeat panels probably will.

Turret speed is not hit rate. The 30 and 40 rpm figures describe how fast the turret rotates to select a tool. They do not tell you how many holes per minute the press punches, and that second number depends on tool spacing and sheet feed. Ask for both.
Two accuracy figures, two meanings. The ±0.1 mm on the JT and SF is machining accuracy. The ±0.01–0.02 mm on the SFL is positioning repeatability of the rack-and-pinion drive. Putting them side by side implies a tenfold gap in part quality that the data does not support. When a supplier quotes accuracy, ask which measure it is and which tolerance standard it follows: ISO 2768 defines general tolerance classes and ISO 286 covers limits and fits.
Sheet size per position. The SFL punches 2500 mm along X in one position and reaches 5000 mm by repositioning. For long switchgear panels the repositioning step is where hole-to-hole error tends to accumulate, so ask how it is handled.
The station total. A turret with more stations is not automatically better if most are the smallest size. Match the map to your tool list.
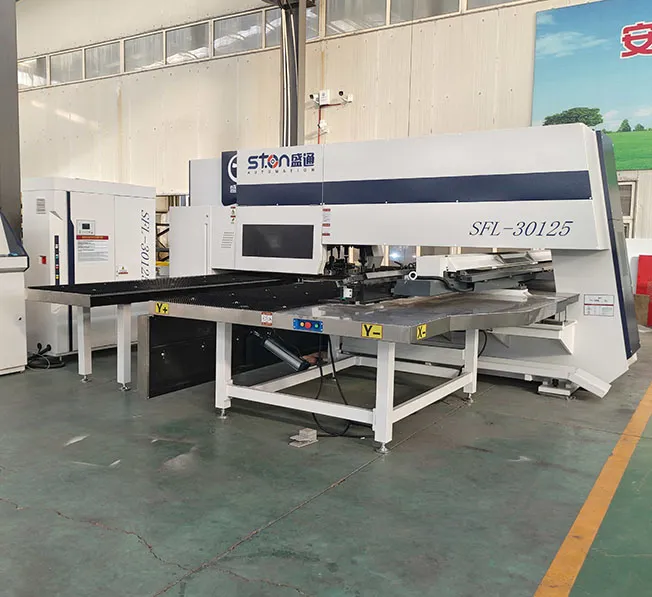
Compared with the common route of buying a turret punch press and a separate laser cutter, a punch-laser combined machine changes the floor plan. STON states that the SFL completes stamping, forming, laser cutting and blanking in a single clamping and takes roughly 40% less space than a separate punch and laser pair. It also removes the handling, secondary clamping and re-alignment between the two.
The cost is concentration. One frame carrying two processes means a fault can stop both, so plants with heavy daily volume on both punching and laser blanking may still prefer two machines. For perforated or louvred panels with a modest share of contour cutting, the combined machine deserves a place on the shortlist.
Equipment dealers and distributors should weigh what sits behind the machine: OEM/ODM customization on modular structures, spare-parts inventory depth, software-update policy and service documentation. Those decide whether you can support an installed machine in your own market without calling the factory for every fault.
Electrical panel factories work with cabinet doors, switchgear panels and ventilation plates. Check the tool map for louvre and rib tools, the sheet travel for your longest panel, and whether the turret pairs with automatic loading and unloading. STON‘s automated line handles sheet separation, positioning, unloading and stacking without an operator.
There is no universal number. List every tool size and rotary tool your parts require, then ask each supplier for its station map by size. STON’s SFL lists 16 A, 11 B, 3 C and 2 D stations.
On STON’s data, the servo SF runs up to 40 rpm and draws roughly 3–5 kW, while the mechanical JT runs up to 30 rpm at 2 kW or less. Both list ±0.1 mm machining accuracy. High-shift repeat work favours the SF, and lighter mixed batches can favour the JT.
Yes, within limits. STON’s turrets handle punching, forming and embossing, and the line configuration adds trimming, louvering and rib pressing. Ask for the forming tool list and maximum forming height before ordering.
Machinery Directive 2006/42/EC governs CE marking, and EN ISO 12100 and EN ISO 13849-1 cover risk assessment and safety-related controls. Request the declaration and technical file.
STON does not list a public price range for the JT, SF or SFL, so a quotation is required. Specify tooling, loading, and freight in the request.



Que vous modernisiez une ligne existante ou que vous lanciez un nouveau projet, STON personnalisera une solution CNC pour votre production.


