Nous sommes responsables de la construction-----nous sommes responsables de la fabrication-----nous sommes responsables de la formation

Panel benders rated for cold-rolled steel don’t bend stainless the same way. On STON’s Press Arm Type line, the full-bend ceiling drops to SS 1.0mm on welded-frame models and SS 1.2mm on cast-frame models — well below the CR 1.5–2.0mm figures most spec sheets lead with.
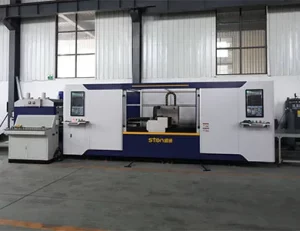
STON’s Press Arm Type cintreuse de panneaux is built in both welded and cast bed configurations, and the two configurations don’t share a thickness ceiling. This is the figure to check before quoting a stainless job, not the generic “up to 2mm” line.
| Modèle | Cadre | Max. Bending Size (mm) | CR Thickness (Full Bend) | SS Thickness (Full Bend) | Servo Axes |
| A (1000) | Welded | 1000 × 1000 | 1.5 mm | 1.0 mm | 15 |
| A+ (1200) | Welded | 1200 × 1200 | 1.5 mm | 1.0 mm | 15 |
| B (1400) | Welded | 1400 × 1250 | 1.5 mm | 1.0 mm | 15 |
| B (1400) | Cast | 1400 × 1250 | 2.0 mm | 1.2 mm | 15 |
| B+ (1600) | Welded | 1600 × 1250 | 1.5 mm | 1.0 mm | 15 |
| B+ (1600) | Cast | 1600 × 1250 | 2.0 mm | 1.2 mm | 15 |
| C (2000) | Welded | 2000 × 1500 | 1.5 mm | 1.0 mm | 15 |
| C (2000) | Cast | 2000 × 1500 | 2.0 mm | 1.2 mm | 15 |
| D (2500) | Welded | 2500 × 1500 | 1.5 mm | 1.0 mm | 15 |
| D (2500) | Cast | 2500 × 1500 | 2.0 mm | 1.2 mm | 15 |
| D+ (2800) | Welded | 2800 × 1500 | 1.5 mm | 1.0 mm | 15 |
| D+ (2800) | Cast | 2800 × 1500 | 2.0 mm | 1.2 mm | 15 |
Two things stand out here. First, cast-frame models carry a genuinely higher SS ceiling than welded ones (1.2mm vs 1.0mm) — the extra rigidity of the cast bed is what buys the extra 0.2mm, not a different servo package. Second, the gap between CR and SS capacity is proportionally larger than most buyers expect: on the same machine, SS capacity sits at roughly two-thirds of the CR figure, not the same number restated for a different material.
For most commercial kitchen enclosure and cabinet work, sheet runs 0.8–1.2mm SS, which fits comfortably on either frame type. Heavier-gauge stainless — thick equipment bases, structural brackets — needs the cast-frame B+ through D+ models, and anything past 1.2mm on a panel bender isn’t a configuration question anymore; it’s outside what this machine class does.

Stainless springs back more than cold-rolled steel after the bend arm releases, because it has a higher yield point relative to its stiffness. On a machine without a real compensation mechanism, this shows up as parts that measure a few degrees off target and require manual rework or a second pass.
The Press Arm Type line addresses this with a compensation rapid adjustment device that lets an operator correct bending accuracy and angle at any point along the bend line without swapping shims. That distinction matters for SS work specifically: shim-based compensation is workable for a CR job that runs unchanged for weeks, but stainless jobs in kitchen equipment tend to mix gauges and part geometries within the same production day. Re-tuning through shims between batches is slow enough that shops either skip it or eat the reject rate. A tool-less adjustment point is what makes per-batch compensation actually happen instead of getting deferred.
This is the edge case most vendor content skips entirely. A polished stainless panel that comes off the bender with a faint line down the fold isn’t a machine capacity failure — it’s a contact-surface failure, and it happens even well within the rated thickness.
Three points worth checking before ordering:
None of this changes the machine’s thickness rating. It changes whether the part passes visual inspection, which for kitchen equipment buyers is often the harder requirement to meet.
Not every stainless kitchen equipment order belongs on a panel bender. STON’s Laser Bending Automatic Production Line — an integrated coil-uncoiling, laser-cutting, and bending line — handles stainless up to 1.5mm, a higher figure than either Press Arm frame type manages. That’s not a contradiction; it’s a different production model. The laser line processes coil stock through cutting and bending in one continuous automated sequence, which suits high-volume, standardized parts — think repeat-run equipment panels at scale — rather than the mixed-geometry, job-shop-style work that a panel bender is built for.
A buyer deciding between the two should be sizing by order pattern, not just by thickness: standardized panels at volume point toward the laser line; varied job orders with frequent changeovers point toward the panel bender, even though its stainless ceiling reads lower on paper.
| Factor | Welded Frame | Cast Frame |
|---|---|---|
| SS Thickness at Full Bend | 1.0 mm | 1.2 mm |
| CR Thickness at Full Bend | 1.5 mm | 2.0 mm |
| Structural Rigidity | Standard | Higher |
| Typical Fit | Lighter-gauge kitchen panels and cabinet doors | Equipment bases, structural brackets and heavier enclosures |
If a job runs consistently at 1.0mm SS or lighter, the welded frame is not under-specified for it — buying the cast frame in that case adds cost without adding usable capacity. The cast frame earns its price when the job regularly touches 1.0–1.2mm.
Stainless-specific issues — springback compensation, tooling surface treatment, correct feeding hardware — are exactly the details that get lost when a machine passes through an intermediary. A trading company reselling equipment it doesn’t build usually can’t answer whether the auxiliary knife on a given unit is rated for polished-finish material, because that’s a manufacturing decision, not a resale one. STON keeps casting, machining, assembly, and inspection in-house across its Qingdao factory, which is what makes it possible to specify tooling and feeding hardware to the material grade at order time.
On STON’s Press Arm Type line, it’s 1.0mm at full bend on welded-frame models and 1.2mm on cast-frame models — not the higher CR figure often shown as the headline spec.
This is springback, and it’s a normal property of stainless, not a defect. It needs to be corrected through the machine’s angle compensation mechanism, ideally one that adjusts without shim changes if the job mixes gauges.
Not if that setup uses magnetic grippers. Austenitic stainless (304/316) is non-magnetic, so feeding needs to be specified with vacuum or mechanical clamping instead.
It depends on the order pattern. The laser bending line handles stainless up to 1.5mm and suits high-volume standardized panels; the panel bender fits varied job-shop work even at its lower 1.0–1.2mm ceiling.



Que vous modernisiez une ligne existante ou que vous lanciez un nouveau projet, STON personnalisera une solution CNC pour votre production.


