Мы отвечаем за строительство----- мы отвечаем за производство----- мы отвечаем за обучение

A ventilation panel punching machine is a CNC turret press that stamps louvres, slots, and grille holes into sheet metal using a rotating die head instead of a cutting beam. For panels with dozens or hundreds of repeated openings, that stamping action produces parts faster than laser cutting because each hole is a single mechanical stroke, not a traced outline.
The core mechanism is a turret loaded with dies — round, louvre, slot, and custom profiles — that rotates a specific tool into position under a ram. The ram strikes, the sheet indexes to the next hole location, and the cycle repeats. STON’s turret punch line covers this application directly: switchgear panels, distribution cabinet doors, and ventilation plates are listed as core use cases for the CNC Turret Punch Press family, alongside forming and embossing work that a pure cutting tool can’t do in the same pass.
This matters for ventilation parts specifically because a louvre panel isn’t really one shape — it’s the same shape repeated 40, 80, or 200 times across a sheet, sometimes in staggered rows for airflow tuning. The production question isn’t “can this machine cut a louvre,” it’s “how many louvres per minute, and how many tool changes does the pattern require.”
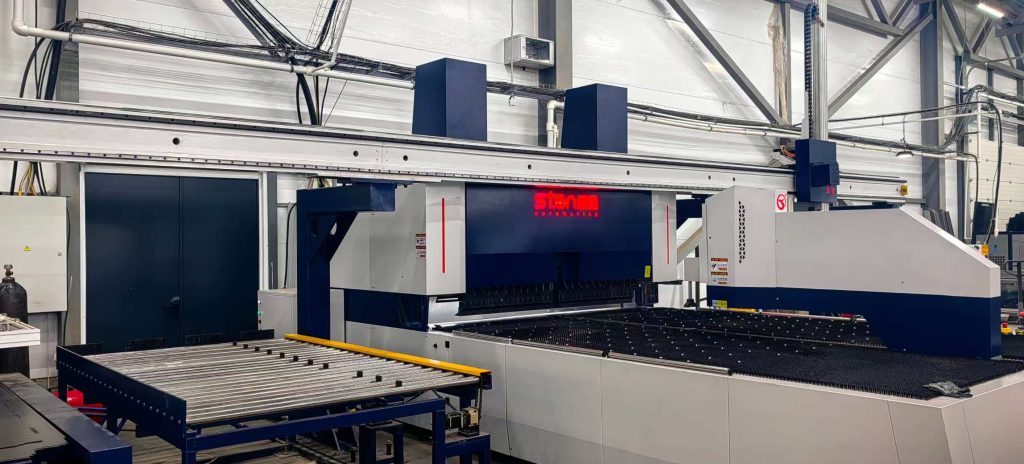
A laser head has to trace the full perimeter of every hole — start point, cutting path, pierce time, retract. A punch press with the right die stamps the entire hole shape in one strike. On a panel where holes are the majority of the geometry rather than the exception, that difference compounds fast.
Compared with a typical stand-alone laser-cutting setup handling the same hole-dense pattern, a turret press removes the per-hole traversal time almost entirely — the tool doesn’t need to travel around a shape’s edge, it lands on it.
The Hit-Rate Math
STON’s punching data gives a concrete anchor for this. On the Серия SFL servo punch-laser combined machine, the punching side has a rated step pitch of 405 strokes per minute. That figure is drawn from STON’s servo punching mechanism specification sheet (SFL Series CNC Servo Punch Laser Combined Machine) rather than the stand-alone turret models, but it reflects the same servo-driven strike cycle used across STON’s punching lineup.
| Параметр | Mechanical CNC Turret (JT Series) | Servo CNC Turret (SF Series) |
| Max. Turret Rotation Speed | 30 об/мин | 40 об/мин |
| Точность обработки | ±0,1 мм | ±0,1 мм |
| Max. Sheet Load Capacity | 150 кг | 150 кг |
| Суммарное энергопотребление | ≤2 кВт | Approximately 3–5 kW |
| Давление источника воздуха | 0,55 МПа | 0,55 МПа |
| Источник питания | 380 В ±5% | 380 В ±5% |
STON’s turret systems are built around a double-chain drive mold system as standard, which keeps die position repeatable over long production runs without the tensioning drift that causes hole placement to drift on a chain-driven turret over time. Two independent rotary workstations (commonly configured as 1B and 1C positions) let the machine hold two different rotating die shapes loaded simultaneously — useful when a ventilation panel calls for both round louvre vents and slotted grille sections without a manual tool change mid-run.
For panels combining punched holes with laser-cut irregular cutouts — a common ventilation-panel request when the enclosure also needs a custom logo cutout or an odd-shaped access port — STON’s SFL combined series handles both processes on one machine, in one clamping. That avoids the secondary alignment step a two-machine (separate punch, separate laser) workflow requires.
Турельная пробивка isn’t the better choice for every ventilation panel job, and treating it as a universal upgrade over laser cutting is a common misreading of the hole-density argument above.
Low-volume or prototype runs don’t benefit from stamping’s per-hole speed advantage, because programming a new die layout — or sourcing a custom die for a non-standard hole shape — costs more setup time than a laser simply tracing a new CAD profile. If a ventilation panel design changes every batch, or the run is under a few dozen pieces, laser cutting’s tool-free flexibility usually wins on total turnaround, even though its per-hole cycle time is slower.
Irregular, freeform ventilation patterns — organic vent shapes, brand-specific perforation art, or one-off architectural louvre panels — also favor laser cutting, since a punch press is limited to the die shapes physically available on the turret.

The mechanical JT-series turret runs a lower turret rotation ceiling (30 rpm) and simpler electrical draw (≤2 kW), which suits shops running high-volume, low-mix ventilation panels — the same one or two hole patterns, repeated. The servo SF-series turret adds rotation speed (40 rpm) and a higher power draw (3–5 kW) in exchange for faster tool-change cycles, which pays off when a panel mixes several hole geometries in one part. The SFL punch-laser combined machine adds a fiber laser head to the same punching platform, aimed at panels that need both stamped holes and cut irregular geometry in a single setup.
None of these three configurations is a strict upgrade over the others — the right pick depends on how uniform the hole pattern is and how often the design changes, not on which machine has the higher spec sheet number.
Pricing for STON‘s turret punch and punch-laser combined lines varies by configuration, tooling package, and automation add-ons — buyers should request a quote against the specific hole pattern and material spec rather than a general price range.
For CE-marked export markets, turret punch presses fall under the EU Machinery Directive 2006/42/EC, which governs the safety documentation and guarding requirements a supplier needs to provide alongside the machine.
Only within the die shapes physically loaded on the turret. Custom dies can be manufactured for a specific profile, but a freeform or one-off irregular cutout is generally faster to produce on a laser, or on a punch-laser combined machine like STON’s SFL series that handles both processes on one platform.
It depends on hole uniformity. A single-die, high-repetition pattern runs closer to the punching mechanism’s stroke-rate ceiling; STON’s SFL punching side is rated at 405 strokes per minute. A mixed-geometry panel spends more cycle time on turret indexing (30–40 rpm depending on model), which narrows the gap with laser cutting.
Yes. STON’s mechanical JT-series draws ≤2 kW combined; the servo SF-series draws roughly 3–5 kW in exchange for a higher turret rotation speed (40 rpm vs. 30 rpm) and faster tool-change cycles.
STON’s standard turret configurations rate a maximum sheet load of 150 kg. Specific material thickness limits depend on hole size, die selection, and sheet material — confirm against your panel spec before ordering.
For sale into the EU, turret punch presses fall under the Machinery Directive 2006/42/EC. Confirm CE documentation and guarding compliance with the supplier before shipment.


Если вы модернизируете существующую линию или начинаете новый проект, STON разработает решение с ЧПУ для вашего производства.


