Somos responsáveis pela construção----- somos responsáveis pelo fabrico----- somos responsáveis pela formação

Automação de chapas metálicas works best in stages: automate loading and unloading first, add automated bending once parts run consistently, then connect uncoiling, laser cutting, punching, and bending into one line. This sequence lets a factory prove ROI at each step before committing capital to a full production line.
A factory manager calls a machine builder, describes wanting to “go automated,” and walks out of the conversation with a quote for a complete uncoiling-to-stacking line. The number is large, the payback period is long, and half the line’s capacity sits idle because the factory’s actual part mix doesn’t need that much throughput yet.
The more workable path starts smaller. Automate the step that’s currently costing the most in labor and part damage — usually loading and unloading — confirm it holds up in daily production, then decide whether the next bottleneck justifies the next piece of equipment. Each stage generates its own data: cycle time, scrap rate, operator hours saved. That data is what should drive the next purchase decision, not a sales quote for everything at once.
This is not an argument against full-line automation. STON builds those lines. It’s an argument for sequencing the investment so a factory isn’t paying for integration complexity it doesn’t need yet.
Loading and unloading is usually the easiest automation entry point because it doesn’t change how the part is formed — it changes how the part gets to and from the machine. Three configurations cover most factory layouts:
| Tipo | Best Fit | What It Solves |
| Robotic Arm | Mixed part sizes and frequent changeovers | Flexible pick points; programmable for multiple part geometries |
| Gantry System | Long production runs and fixed part families | Consistent overhead travel path; reduced floor footprint per station |
| Truss-Type Manipulator | High-volume, single-line feeding | Continuous material flow between adjacent stations |
The benefit isn’t just labor reduction. Manual loading and unloading is where panel edges get scratched, corners get dented, and operators get closest to pinch points on the press. Removing that step reduces part damage and improves machine utilization, since the machine isn’t waiting on a person between cycles.
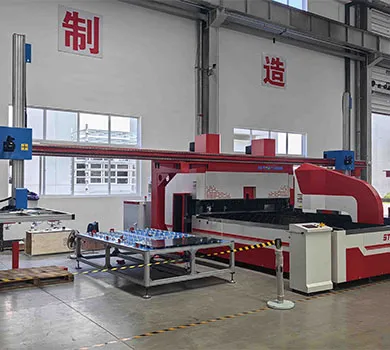
Automated loading only pays off if the part coming off the previous station is positioned the same way every time. That’s the real prerequisite for stage 2, not machine budget.
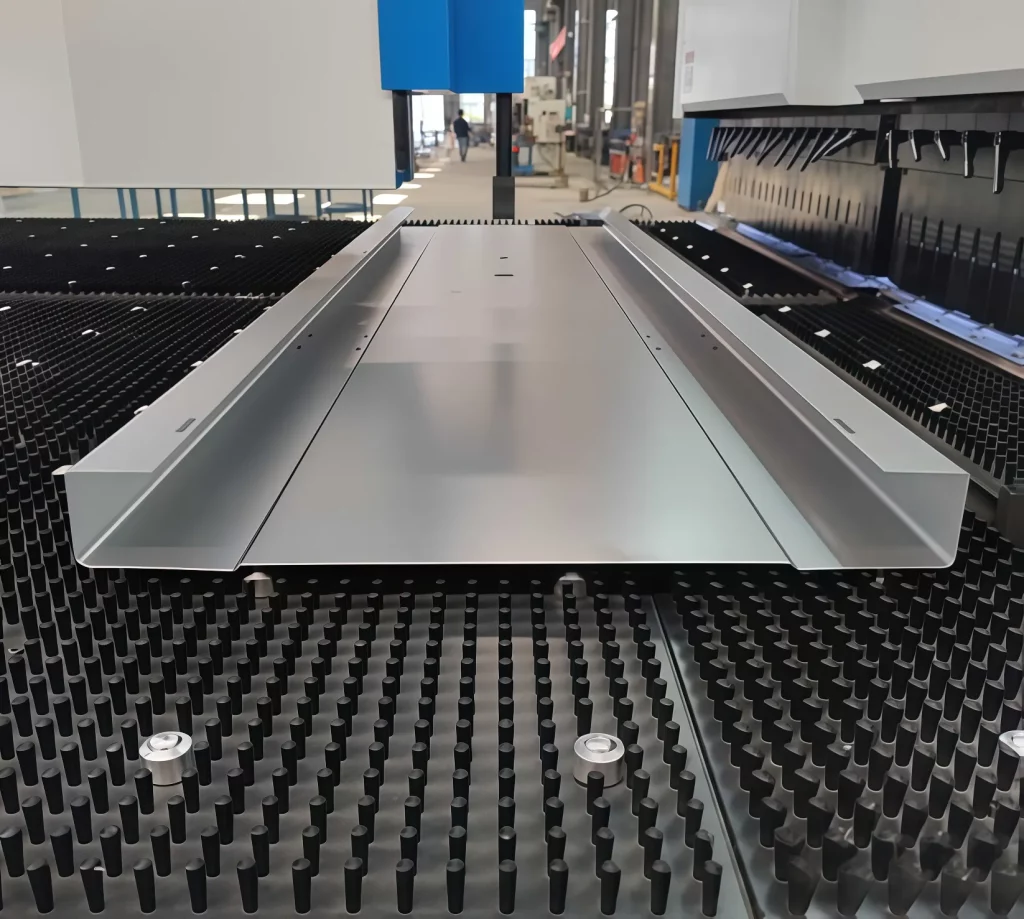
Once loading is stable, the next candidate is usually the panel bender. STON’s flexible edge bending machines are available with automatic loading and unloading built into the bending cycle, not bolted on afterward — the machine’s docking port and the loading unit’s feed path are matched at the design stage.
| Modelo | Max Forming Size (mm) | Max Forming Inner Dimension for Auto Load/Unload (mm) | Min Bending Height (mm) |
|---|---|---|---|
| 1200 | 1200 × 1200 | 1200 × 650 | 4 |
| 1600 | 1600 × 1250 | 1600 × 950 | 4 |
| 2000 | 2000 × 1500 | 2000 × 800 | 4 |
Note the gap between “max forming size” and “max forming inner dimension for auto load/unload” — a 2000mm bender can still form a full 2000×1500mm panel manually, but the automated feed path only handles up to 2000×800mm. This is a real constraint, not a marketing footnote: if a factory’s typical part exceeds the automated dimension, the bender still needs manual intervention for that part family even after the automation upgrade. Confirm actual part dimensions against this table before assuming full automation coverage.
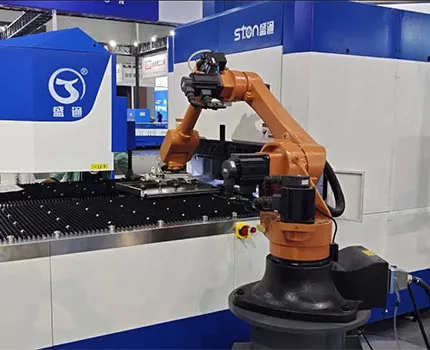
Full-line automation links uncoiling, leveling, laser cutting, CNC punching, automated bending, and — where needed — a robotic welding workstation into one controlled sequence. This is where the capital commitment jumps, and where it should only happen after stages 1 and 2 have already proven out on the shop floor.
The uncoiling-leveling-laser-cutting stage alone carries its own parameter set that determines what the rest of the line can run:
| Parâmetro | Valor |
| Matéria-prima | Cold-rolled sheet, galvanized sheet, stainless steel |
| Espessura da chapa | 0.5–2.0 mm |
| Largura da placa | 1000–1500 mm |
| Roll Weight | ≤10 T |
| Precisão de nivelamento | ±1 mm/m² |
| Precisão diagonal | ≤1 mm/2000 mm |
| Velocidade de rosca | 5 m/min |
| Unit Linear Speed | 0–12 m/min (adjustable) |
Downstream of leveling, the Prensa de punção de torre CNC with its own loading and unloading unit handles punching, trimming, forming, and rib pressing before the part reaches the bender. If welding is part of the process — cabinet corners, enclosure seams — a welding robot with positioner and seam-tracking can be added at the end of the sequence, though this is the piece most factories add last, once the upstream stations are already running unattended.
| Dimensão | Staged Rollout | Full Line from Day One |
| Capital Committed Upfront | Low at Stage 1; grows with proven need | High, regardless of near-term part mix |
| Time to First Measurable ROI | Weeks—based on loading/unloading data | Months—the whole line must be commissioned before output stabilizes |
| Flexibility if Part Mix Shifts | Easier—swap or reconfigure one station | Harder—line balance was engineered around the original part mix |
| In-House Skill Required | Grows gradually with each stage | Needed all at once during commissioning |
| Downtime Risk from a Single Fault | Isolated to one station | Can stop the whole line, depending on buffer design |
Compared with buying a complete turnkey line up front — the common sales pitch in this category — the staged approach trades some line-level efficiency (a fully synchronized line can outrun the sum of its separately-added parts) for lower risk and faster feedback on whether the automation investment is actually paying off for that factory’s specific part mix.
It depends on whether the existing bender has a compatible docking interface. STON’s units are designed to interface with most robotic arms and gantry systems already on the market, but retrofitting an older machine without a docking port may require additional integration work — confirm with the equipment supplier before ordering the automation unit.
Yes, in most cases. Adding robotic loading/unloading to an existing machine changes the equipment’s risk profile, which under EN ISO 12100 (machinery risk assessment) and EN ISO 13849-1 (safety-related control systems) typically requires a fresh risk assessment of the combined system — not just relying on the new unit’s own CE marking. This matters specifically for EU-bound installations under Machinery Directive 2006/42/EC.
There’s no fixed timeline — it depends on how quickly loading/unloading data confirms ROI and how fast the next bottleneck becomes clear. Some factories run stage 1 for a full production cycle before deciding on stage 2; others move within weeks if the labor and part-damage savings are obvious immediately.
The gap between a bender’s max forming size and its max forming inner dimension for automatic loading/unloading (see the table above). A part can be within the bender’s forming capacity but still fall outside what the automated feed path handles.



Quer esteja a atualizar uma linha existente ou a iniciar um novo projeto, a STON personalizará uma solução CNC para a sua produção.


